Intelligent Video Analytics Software Adoption Trends Across Discrete and Process Manufacturing
Jeff Zeller | September 9th, 2026
A defect that clears one station and surfaces three stations later carries a cost you can put a number on: scrap, rework, a quality hold on everything built since the last known-good unit, and an argument with a customer about containment. That consequence is what drives most first conversations about intelligent video analytics software, and it is also where evaluation gets harder than buyers expect. The published record on this software category is organized around security, perimeter, and investigation use cases, so a shortlist built from vendor material tells you a great deal about intrusion detection and very little about whether a platform holds up on a stamping line or in a facility where steam drifts across the camera’s field of view for half the shift.
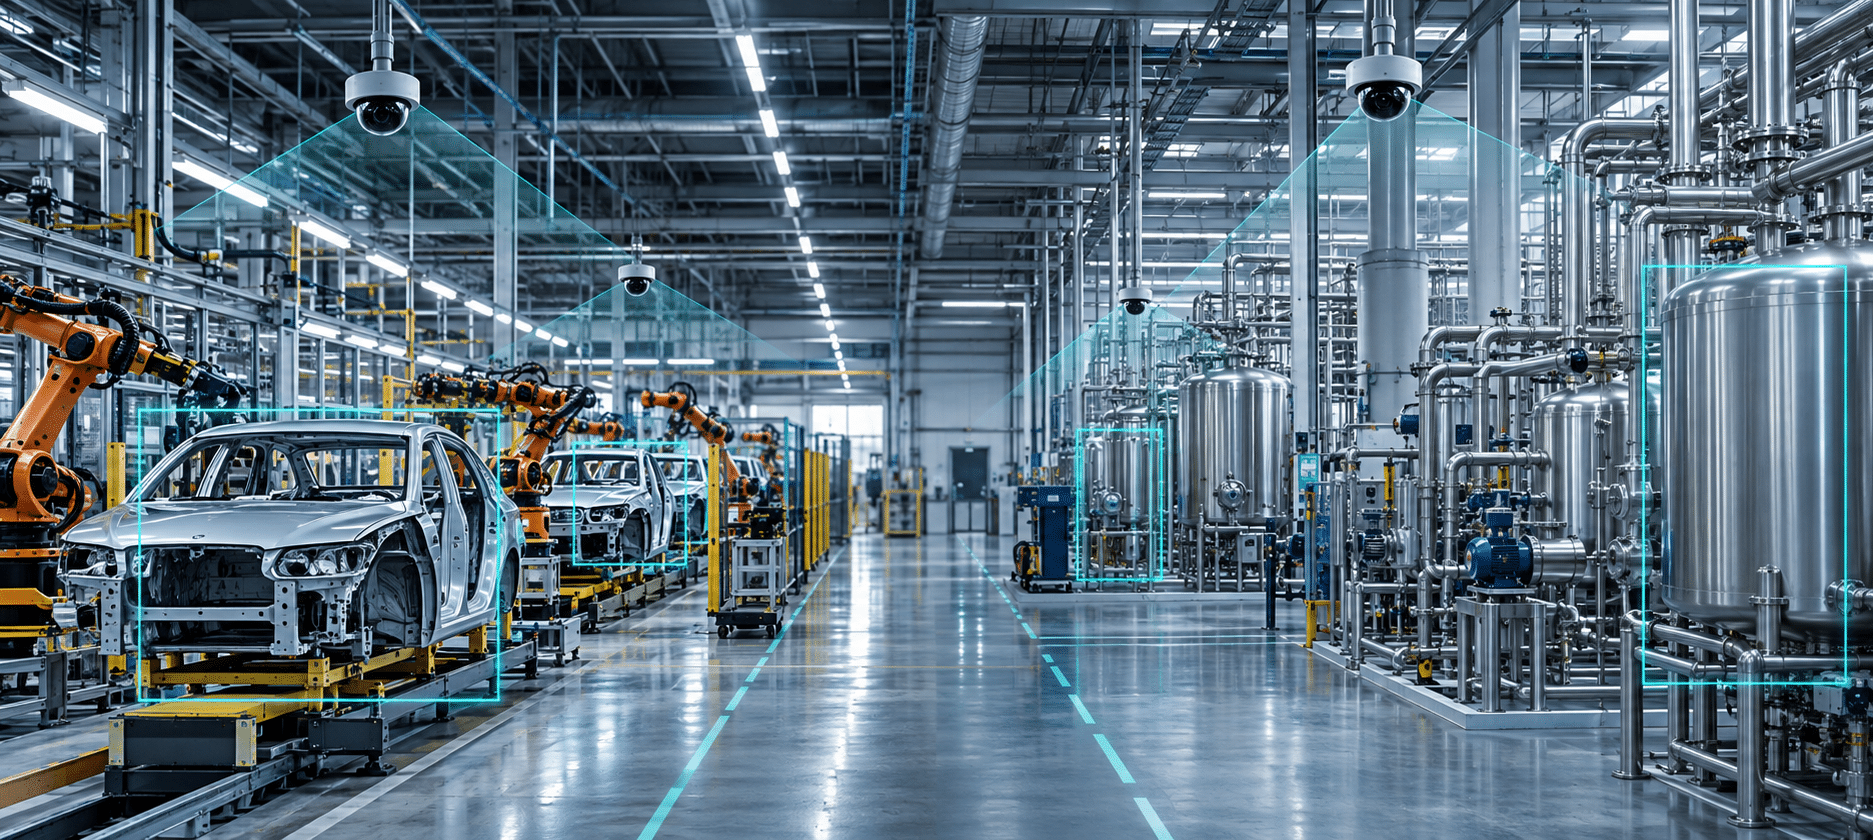
Discrete and process manufacturing place different demands on the same software, and the difference shows up in every technical decision that follows: whether detection is rule-based or learned, whether inference runs at the camera or in the cloud, and whether analytics output lands in a security dashboard or in the systems your quality and operations teams already use. What follows is an assessment of where adoption evidence is strong enough to act on, where it is thin enough that you should require disclosure from a vendor, and how the two manufacturing modes diverge in practice.
Where Adoption Data Is Solid and Where It Runs Thin
Security applications are the best documented part of this market by a wide margin. Multiple vendor sources describe perimeter monitoring, loitering discrimination, and post-event investigation in operational detail, with named products, configurable rule behavior, and customer language attached. Quality inspection and process monitoring appear in the same material, but usually as a bullet in a use case list rather than as a deployment with figures behind it, which means the evidence supporting operational monitoring is qualitative where the evidence supporting security is specific.
The second gap matters more for a manufacturing buyer. Published sources treat manufacturing as a single vertical, frequently bundled with logistics and warehousing, and none of them disaggregate adoption between discrete production and continuous process production. Testimonial evidence has the same limitation: OpenEye’s own material carries a customer praising how easy the product is to use, which is worth something as a usability signal and nothing at all as a measure of how many plants of a given type are running analytics in production. With no sub-vertical adoption figures available anywhere in the public record, the honest method is inference from deployment patterns and feature emphasis, reading what vendors chose to build and document as a proxy for where their customers actually are.
Rule-Based versus Machine-Learning Analytics in Manufacturing Contexts
The architectural split running through this category is older than the current wave of marketing. Rule-based analytics fire on fixed geometric triggers: a line crossed, a zone entered, an object dwelling longer than a configured threshold. Milestone’s material describes exactly this logic in a security frame, explaining that specific rules can distinguish ordinary behavior from loitering, and the approach works well when the scene is stable and the event of interest is defined by position. Move that same logic onto a plant floor where lighting shifts, fixtures get repositioned, and material handling equipment moves through the frame all day, and fixed triggers produce false positives at a rate that trains operators to ignore the alerts.
Discrete manufacturing gives learned models a friendlier problem: part geometry repeats, camera angles are fixed at the station, and the difference between a good assembly and a bad one is visually consistent from unit to unit. Machine-learning classification in that setting supports defect detection and assembly verification without an engineer rewriting rules every time a fixture or a product variant changes. Process manufacturing is the harder case, because continuous flow, variable occlusion, and interference from steam or particulate make the visual baseline itself unstable, and a model trained under one set of conditions can degrade when those conditions shift.
Retraining cadence therefore belongs in your procurement criteria rather than in a post-purchase conversation. Matroid’s platform includes a custom detector studio, MLOps architecture, quick training, and analytics from video streams, and the MLOps layer is the part that matters here, because a detector that can be retrained on new footage by the team that owns the process is a different operational proposition than one that requires a vendor engagement each time the scene changes. No-code creation lowers the barrier to building detectors; it does not remove the need for technical oversight of how those detectors are validated and maintained. Vendor provenance is worth reading with the same eye. Irisity’s IRIS+ platform is presented as an AI-based system built on a scalable IoT architecture drawing on twenty years of experience, and architectural maturity of that kind tells you about the engineering lineage without telling you how the models behave on your specific defect classes.
Discrete Manufacturing Uptake Patterns
Discrete production aligns almost point for point with the feature set that video analytics vendors have built. Automotive assembly and electronics fabrication run fixed-station workflows where the camera sees the same part in the same orientation thousands of times per shift, which is the condition under which object detection, presence and absence checks, and assembly verification are most tractable. Repetitive part geometry also shortens the path to a working detector, because the training set covers the range of variation the model will actually encounter rather than a fraction of it. Faster training and fewer confounding variables are not a guarantee of performance on any particular defect, and any serious evaluation still ends with testing on your own footage, but the starting position is favorable.
Camera infrastructure is the practical constraint in most discrete plants, where the estate is mixed: analog cameras installed years ago for general area coverage, newer IP cameras added for a specific project, and sometimes machine vision cameras dedicated to a single inspection task. Platforms that work with existing hardware avoid turning an analytics project into a capital project. Matroid says its software works with any image or video hardware, and camera-agnostic deployment of that kind reduces integration friction precisely where discrete manufacturers tend to stall, which is the moment someone prices a full camera replacement against an uncertain return.
What you will not find is a published source that isolates discrete-only adoption. Vendor documentation groups logistics and manufacturing together, counts deployments across industries rather than within them, and rarely separates a defect inspection installation from a dock door monitoring installation. Feature emphasis remains the most reliable signal available: when a vendor invests in object detection, classification, and event analytics on production footage, discrete customers are usually the reason.
Process Manufacturing Uptake Patterns
Process facilities ask the software a different question. Instead of inspecting a part, analytics in a chemical plant, refinery, food processing line, or pharmaceutical facility watches zones, behaviors, and hazard conditions: whether a restricted area is occupied, whether a spill or leak has appeared, whether a task is being performed in the sequence the SOP specifies. Axxonsoft’s published feature set maps onto that reality with smoke and fire detection and posture analytics, capabilities that make sense in a facility where the earliest visible sign of a problem is environmental rather than dimensional.
The environment is also what makes process deployments harder to sustain. Steam, dust, particulate, condensation on lenses, and low-light areas raise the rate at which models fail or produce ambiguous output, and each of those conditions varies with season, product run, and equipment state, which pushes retraining from an occasional maintenance task toward a scheduled one. Matroid says users can detect and classify defects, objects, assemblies, hazards, and events, and hazard and event detection is the natural fit for process environments, provided the deployment plan accounts for a visual baseline that will not hold still.
Worker monitoring in hazardous roles carries a separate set of constraints that has nothing to do with model performance. Posture analytics and behavior detection touch employment law, works council agreements, privacy regulation, and internal labor relations, and the scope of what gets monitored, retained, and reviewed should go through legal and compliance review before any camera is pointed at a person rather than after. Analytics of this kind supports safety and compliance programs by surfacing conditions faster; the judgment about whether a condition is acceptable, and what to do about it, stays with the people accountable for it.
Where Published Sources Disagree and Why
The asymmetry in the published record has a straightforward cause: most vendors in this category entered manufacturing through the security channel. They sold to facilities and security teams first, built documentation and case studies for those buyers, and later extended the same platforms toward quality and operations. Security documentation is consequently mature and specific, while operational-monitoring documentation reads as aspirational, and the disagreement between sources is less a factual dispute than a difference in what each one was written to sell.
Scale figures illustrate the problem. Intellivision’s products are described as running in over seven million cameras globally, largely through OEM and integrator relationships, and the number is real without being usable as a manufacturing adoption metric, since nothing in it separates industrial installations from retail, residential, or municipal ones, let alone discrete plants from process plants. Milestone makes a broader operational argument, noting that Video intelligence has applications far beyond security. Management can make significant operational improvements by tracking variables such as customer and employee behavior. Directional claims of that kind are useful for understanding where the category is heading and useless for comparing sub-verticals, because no quantification accompanies them.
Comparative roundups add a third register. One vendor profile pairs a ten-year hardware warranty against notes that the option is costly and architecturally built on proprietary cameras with fixed processing capabilities, which is buying advice rather than adoption data, though the proprietary hardware constraint it identifies has direct consequences for manufacturing sites, as the next section takes up.
Edge versus Cloud Processing in Industrial Deployments
Where inference runs is dictated by what happens after a detection. High-throughput discrete inspection with a rejection window measured in fractions of a second needs the decision made locally, because a round trip to a cloud endpoint introduces variable latency that no amount of bandwidth reliably removes, and a reject actuator that fires late is worse than no actuator at all. Edge processing is the default for closed-loop inspection and for anything that triggers equipment.
Process facilities have more room to choose. Compliance monitoring, SOP conformance review, incident reconstruction, and trend analysis across shifts tolerate seconds or minutes of delay, so cloud processing is viable and often cheaper to stand up across a large site with many low-frame-rate views. The cost structures differ rather than one being cheaper outright: edge deployment means compute hardware at or near each camera node and an upfront capital line, while cloud deployment converts that into ongoing bandwidth and storage spend that scales with how many streams you keep and how long you retain them.
Regulated process industries add a constraint that can settle the question before economics do. When footage captures proprietary formulations, controlled processes, or identifiable workers, moving it off premises triggers data sovereignty and residency review, and pharmaceutical, food, and defense-adjacent facilities routinely find that the review takes longer than the deployment would have. Deployment flexibility is worth evaluating as seriously as detection capability, because a platform that only runs one way will eventually meet a site where that way is not permitted.
Integration with Existing Camera Infrastructure and VMS Platforms
Proprietary camera requirements are the most common hidden cost in this category. When a platform’s architecture depends on the vendor’s own cameras with fixed processing capabilities, as one option in the published comparisons does, the entry price includes replacing hardware that is currently working, and facilities with large legacy camera estates tend to defer the project rather than fund the replacement. Camera-agnostic platforms invert that calculation by treating the existing estate as the input, which both lowers the cost of a first deployment and keeps the door open to expanding across mixed hardware later. Matroid says its software works with any image or video hardware, and in a plant running three generations of cameras, that flexibility is the difference between a pilot at one station and a path to the whole line.
Video management systems are the other integration surface. Most manufacturing sites already run a VMS for recording and retrieval, and buyers need to decide deliberately whether analytics should be embedded in that platform or run alongside it, because the choice determines who administers detectors, where alerts are configured, and how much of your analytics roadmap is bounded by your VMS vendor’s release cycle. Embedded analytics is simpler to operate and narrower in what it can detect; standalone platforms give you more modeling freedom and one more system to manage.
The integration decision that most often destroys the business case is quieter than either of those. When analytics output routes exclusively to a security dashboard, the alerts reach a team with no authority over production, and the operational value never materializes: no defect record enters the quality system, no event correlates to a work order, no trend reaches the engineer who could change the process. Getting detection results into the MES, quality management system, or historian is what converts a monitoring deployment into a manufacturing improvement, and it is worth scoping in the first phase rather than the third.
What Adoption Justifies Acting On Now versus Waiting On
Some use cases are supported well enough by the published record and by current platform capability that delay is hard to justify. Perimeter and restricted-zone detection, object presence and absence checks, and assembly verification in discrete production sit on documented vendor capability, work with existing cameras where the platform is camera-agnostic, and produce results a plant can evaluate in weeks. Incident review is the fastest of them all: Milestone reports that with analytics of this kind, post-event investigations that took hours or even days now take minutes, and the same compression applies directly to reviewing a line stoppage, a containment event, or a near miss on a discrete line, where the alternative is an engineer scrubbing through recorded footage.
Other decisions deserve patience and specific disclosure from vendors. Process environments with steam, particulate, or persistent low light have no published model performance benchmarks behind them, so ask any vendor to demonstrate detection on footage from your own worst conditions rather than on a reference dataset, and ask what retraining a degraded detector requires in labor and elapsed time. Worker behavior and posture monitoring should wait on legal and compliance sign-off regardless of how quickly the technology could be deployed. Broad quality inspection across a high-mix, low-volume line deserves a scoped proof of concept before a site-wide commitment, because visual variation is the variable that determines feasibility and no adoption statistic can answer it for your parts.
Before either path, settle the question that no published source addresses at all: who owns the analytics after deployment. Someone has to create and version detectors, review flagged events, decide what threshold justifies stopping a line, and fold the results into an existing quality or safety workflow. Organizational readiness of that kind precedes platform selection and is independent of it, and plants that skip the question end up with accurate detections nobody acts on. When a vendor’s architecture supports a scoped test, the practical sequence is to run a proof of concept on your own streams at one station, define in advance what result would justify expansion, and require that the pilot produce evidence in the systems your operations team already reviews.
A short list of what to require from any shortlisted vendor before committing:
- Detection results on your footage, from your hardest lighting and interference conditions, not on a reference dataset.
- A clear account of retraining: who performs it, what it costs in time, and how model changes are versioned and validated.
- Deployment options at the edge and in the cloud, with a documented answer on where footage and inference data reside.
- Integration paths into your VMS and into the quality, MES, or historian systems that will consume the output.
Adoption evidence in this category will keep improving, but waiting for a clean sub-vertical benchmark that no one currently publishes is a poor reason to keep manual visual review in place where it is already slow, expensive, or inconsistent. Matroid’s platform, with its custom detector studio, MLOps architecture, quick training, and analytics from video streams, is built for teams that want to test that proposition on their own footage rather than argue about it in the abstract. Get a demo and start with the station where the cost of a missed defect is easiest to measure.
TL;DR: A defect that clears one station and surfaces three stations later carries a cost you can put a number on: scrap, rework, a quality hold on everything built since the last known-good unit, and an argument with a customer about containment.
Building Custom Computer Vision Models with Matroid
Dive into the world of personalized computer vision models with Matroid's comprehensive guide – click to download today